downloadGroupGroupnoun_press release_995423_000000 copyGroupnoun_Feed_96767_000000Group 19noun_pictures_1817522_000000Member company iconResource item iconStore item iconGroup 19Group 19noun_Photo_2085192_000000 Copynoun_presentation_2096081_000000Group 19Group Copy 7noun_webinar_692730_000000Path
Skip to main content
Default Banner Image

Technology and Trends

Incize has been active in characterization for RF-SOI since its creation in 2014, what are your insights on the RF-SOI industry and 5G technology today?Today, the number of foundries developing switches on RF-SOI is increasing, and this trend will continue for the next few years. We saw this opportunity a while back and invested in it. There is no current viable competition for RF-SOI – nothing will replace it in the short term. There are other technologies, but to replace RF-SOI, this is something only imaginable on the long term. It is a stable market with high demand. Other components of the Front-End-Module (FEM) are also moving to engineered substrates (SOI), and Incize enables its customers to develop these technologies. For the foundries wishing to introduce new engineered substrate (SOI), we help understand the physics behind the technology so that they can migrate to SOI. We help develop test structures and evaluate the technology. From conception to product launch, Incize is the partner of technology enablement. Concerning the 5G market, we see other engineered substrates that will surely appear on the market in the long term, this is why we also highly invest in R D to uncover the next generation engineered substrates and be ready to help our clients with this integration. What is Incize’s added value for customers? Starting as a spin-off from ‘Université Catholique de Louvain’, and established in 2014, Incize’s debut focused on characterization of SOI technology. Today, Incize has enlarged its service portfolio and can be characterized as a technology enabler and partner for engineered substrates and RF technologies. We believe RF is an art and we help you to see the whole picture. Incize customers are wafer suppliers, foundries and fabless companies. The services we offer are testing and modeling of materials and devices used for Radio Frequency (RF) applications. Depending on the use of the substrates, we realize tailored testing and modeling to improve the technology and tune processes. Although big players have teams devoted to this, thanks to our expertise built up over the years our added value is to undertake advanced tests and modeling that customers can not do; with RF SOI being one of our specialties. Incize has seen a steady year-on-year growth and today is built up of a team of 10 full time employees dedicated to finding the solutions to our customer’s problems. 3. Could you please tell us more about Incize's R D capability and state-of-the-art technologies in getting ready for 5G? Incize is also very active in research and development in order to continuously stay ahead of the game and provide innovative and state-of-the-art solutions to our clients. 5G is at the verge of tomorrow, although still not well defined (especially for the mmWave band), requirements are getting more challenging. Once the technology is well understood it can be implemented. Foundries and fabless need our help to do it fast and do it well. It is by working together that we will create great value. Currently we have 7 ongoing research projects. Our research projects address new materials as well as new challenges in design and characterization for 5G communications systems/technologies and beyond. New materials required to fulfill the stringent requirements imposed by the 5G standards are being investigated. Phase changing materials, piezoelectric materials, porous silicon and III-V materials will be incorporated in the new generations of front-end-modules which will be part of the mainstream RF electronic industry on the long run. Our projects are tailored to investigate the performance of these materials as part of the next generation of substrates and to develop appropriate characterization techniques to benchmark state-of-the-art 5G devices. Porous Silicon has been largely studied at Incize and we now offer our customers a complete solution from idea to prototype. For our clients we realize feasibility studies, R D, characterization, modeling and prototyping. We carry out various customizable process in a R D technological platform dedicated to microfabrication. Whether you wish to integrate porous silicon before or after the fabrication of devices, Incize is your dedicated partner. We have also been actively researching piezoelectric materials such as quartz, LiNbO3, LiTaO3, ZnO and more in order to fully understand their properties. We have been actively studying new characterization techniques for this fast-growing market. Whether you want to characterize or simulate piezoelectric materials Incize can help you in this trajectory. One of our research projects is specifically centered on RF-MEMS (Radio Frequency-Micro ElectroMechanical Systems), it aims to increase the skills of Incize in the fields of experimental characterization of these devices. Given the heterogeneous nature of MEMS, the test system must be as complete as possible in order to be able to monitor and collect amaximum of data on the various parameters of the component. RF-MEMS technology can be portrayed as an enabling solution to realise the high-performance and highly-reconfigurable passive components that future 5G communication standards will demand for. Incize will develop not only a RF-MEMS component test service, but also commercial test solutions for manufacturers of MEMS-RF components in order to speed up qualification on production lines. Incize is ready to embark on the road ahead to 5G technologies and beyond.
Read More
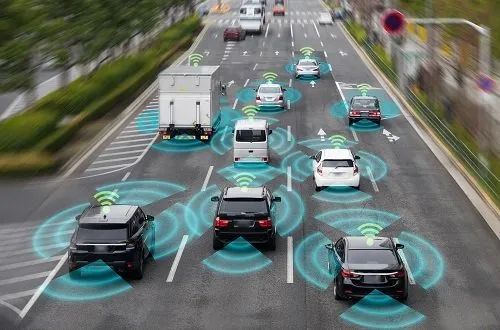
Call it a wild guess, but I suspect I am not the only follower of the automotive industry who is tired of reading articles that lament the impact of Covid-19 and speculate, to varying degrees of accuracy, what kind of recovery is in store for major automotive markets around the world.I’m much more interested in what solutions and creative approaches people, companies, and countries have come up with to make cars smarter and safer despite the pandemic or even because of it.A friend of mine who works at a major European vehicle OEM told me that “innovation cannot, must not stop – despite current difficulties.” This sentiment echoes through the automotive supply chain, particularly in the resilience of the semiconductor industry during these challenging times.The recent publication of the AspenCore Guide to Sensors in Automotive – Making Cars See and Think Ahead is a refreshingly positive and inspiring collection of articles, interviews, technology deep dives and business news, all carefully curated and edited by AspenCore Global Editor-in-Chief Junko Yoshida.One article I particularly enjoyed was her “6 Trends on ‘Perception’ for ADAS/AV.” The insights she was able to gather from experts attending the AutoSens show in Brussels are fascinating, even if consensus on what, exactly, will be the winning “robust perception” solution appears to be far off. This is only fitting with so many companies elbowing for that prime spot!Another feature article that stood out was Nitin Dahad’s “Level 5 AVs Unlikely Before 2035” article. It wasn’t so much the longer ramp to full autonomy that caught my eye but the daunting challenge the automotive industry and AVs have to tackle: “…all possible unusual driving situations under all driving conditions and in all environments.” This is truly a mind-boggling undertaking. The author argues that the road to Level 5 “is likely to be paved gradually, as more advanced driver-assistance features come to market.” Sounds reasonable.Both these articles point to the need for collaboration across the automotive electronics supply chain in order to not only sustain the pace of innovation, but accelerate it, as we face our current challenges. This made me think about the SEMI Smart Mobility initiative and how the great minds supporting it might be able to help. The initiative is designed to bring together automotive OEMs, Tier 1s, device makers, design houses, equipment and materials companies as well as R D institutes to address shared challenges and opportunities.SEMI used to stand for Semiconductor Equipment and Materials International, but over the past several years – and driven by the advent of IoT, AI, and everything “smart” – we now represent the entire electronics manufacturing and design ecosystem, with more than 2,400 member companies on our global roster. We created the Smart Mobility initiative in late 2017 with the initial goal of connecting a substantial number of members to new business opportunities involving rapidly rising silicon content in automotive. IHS Markit projects automotive semiconductor revenue to continue to grow at a 6% CAGR to 2026.Over the past 2 ½ years, the initiative has quickly evolved into a global platform connecting the semiconductor, sensor and automotive electronics ecosystem under one roof – the Global Automotive Advisory Council or GAAC. While “silicon content” is still the operative word for many of our core members, the Council’s mission is to address opportunities and challenges that impact more than one segment of the value chain. For example, the challenge of getting to zero defects involves just about every stakeholder – from contamination control in wafer carriers to ensuring device reliability and robustness to packaging and, ultimately, system integration in the car.SEMI also encompasses a number of Technology Communities that provide deep technical expertise in support of the GAAC’s mission. Member companies in our MEMS Sensors Industry Group (MSIG) are directly engaged in and contributing to the GAAC work. GAAC Europe Chapter - Participating Companies“Sensorizing” – making things smarter through the application of sensors – has created solutions for the automotive and mobility space that bring innovation, safety, security and comfort to driver and passenger and that benefit the environment around the car.This makes the AspenCore Guide to Sensors in Automotive a great resource for our members and SEMI staff as we collaborate to accelerate the drive toward Level 5 autonomy.If you are interested in learning more about SEMI’s Smart Mobility and the GAAC, please contact Bettina Weiss, Chief of Staff and Global Smart Mobility Lead at [email protected] with permission from EE Times.
Read More
I recently spoke with Chan Pin CHONG, Executive Vice President and General Manager of Products and Solutions at Kulicke Soffa, about how smart manufacturing is driving new production efficiencies in the semiconductor industry. During our conversation, he also provided practical steps for factory operators to follow in evaluating their smart manufacturing needs in order to ensure successful implementation and discussed the potential payoffs. Based in Singapore, Kulicke Soffa is a leading global provider of ball bonding, advanced packaging, wedge bonding, and electronic assembly equipment for the semiconductor, power and automotive industries.Ng: Industry 4.0 and smart manufacturing are critical to the growth of the semiconductor industry. What does the smart manufacturing movement mean to you or Kulicke Soffa?Chong: The future of smart manufacturing is the vision of building a digital connected factory to drive new manufacturing efficiencies by combining physical and cyber technologies. Industry 4.0 integrates discrete systems and harnesses the power of large volumes of data to move towards greater automation.At K S, we define smart manufacturing across the following four key areas embedded in our roadmap for all K S products, from wire bonders and advance placement tools to pick and place machines: Interoperability – This is about machines, devices and sensors connecting to each other. In fact, the very basis of smart manufacturing is that all devices are connected. Information transparency – Through simulation, various artificial intelligence (AI) tools use contextual information to emulate the actual world. Technical assistance – Robots or machines support humans in making decisions or solving problems. Autonomous decision-making – This is our vision that robots or machines can learn from machines to make decisions on their own. Ng: Please elaborate on some of these areas and how they’re the relevant to smart manufacturing. Chong: The need for machines, devices and people to communicate with each other forms the basis of connectivity, the idea of all machines communicating with each other or a host. Connectivity protocols now in place for machine-to-machine connectivity include SEMA, SECS/GEM, SEMI-ELS and IPC-CFX. Machine technology uses various sensing technologies. For example, for a pick and place machine such as SMT platform on K S Hybrid, the algorithm to recognize and align processes is part of the sensor needed in each machine before to can process and add thousands of components to the substrate or panel. In a wire bonder, the ultrasonics or EFO signal can provide some form of sensing technology for a machine to detect process conditions. Importantly, these sensing technologies can be used to collect feedback for process improvements.One example of how K S machines are connected to the host is our use of an intermediate server or host named KNeXt to connects to all assembly equipment in the fab. The equipment can then, in turn, connect to an external secured cloud or K S Global Cloud.Ng: What are the objectives for smart manufacturing?Chong: The ultimate goal is to achieve higher factory productivity or better OEE (Overall Equipment Effectiveness) by improving machine yields, productivity and efficiency. The key is to leverage AI, 5G, the Internet of Things (Iot) and other industry 4.0 technologies to drive automation and process improvements. Ultimately, each factory must meet productivity, yield and cost goals. Smart manufacturing enables factory operators to meet these goals. That is the focus of smart manufacturing.Ng: What is the biggest potential benefit of smart manufacturing?Chong: Smart manufacturing uses data to predict outcomes of a process step or machine operation. Once data is available in the global cloud, analytics can start to build data sets to run statistical modelling and examine factory operation trends. We can also use the data to identify past machine behaviors in order anticipate outcomes, including undesirable ones that we can then prevent.In the SMT example, if we can systematically examine days or weeks of historical performance, we can plot some statistical variations in the process specifically to a pick or placer or a robot and anticipate or avoid problems. However, all sensors must be in place in the bond head or the robot so that we can detect changes or variations in the robot’s movements.Kulicke Soffa smart manufacturing facility Ng: What are some recent factory improvements smart manufacturing has enabled? Chong: Kulicke Soffa has contributed to the hierarchical architecture of the smart factory and key technologies. COVID-19 is driving demand for greater factory connectivity, and K S offers solutions that are key to remote management and full control of smart equipment from a central control and embedding Internet of Things (IoT), big data, cloud computing and sensors in manufacturing. Using these technologies, a small smart factory can be remotely operated and managed.With COVID-19 limiting air travel around the world and access to support engineers, the need has grown for remote machine access to reduce the downtime per machine. Remote factory access enables off-site engineers to remotely identify and diagnose machine problems.Ng: What are barriers to faster adoption of smart factories?Chong: While most smart factories are capable of network connectivity and data collection, a key challenge is the lack of a business model for smart factories and smart equipment. Most factories must justify major capital investments by demonstrating ROI (Return of investments) potential. Capital improvements for every factory usually take several years to implement and are based on a complex business model. Factory connectivity requires substantial investments and years to implement. The same is true of the cloud infrastructure buildouts necessary to generate big data and meaningful analytics. The executive mandate for factory management to install capability usually calls for specific business targets in the planning stage.Another longstanding barrier to entry is the lack of compatibility of existing tools with new factory protocols, raising the question of whether the cost of replacing legacy tools justifies the need for a smart factory. If new factory investment is required for the latest tools to support the production of new products, the ROI will be much easier to justify.Ng: How is AI is important in smart manufacturing?Chong: AI interprets and learn from data to perform tasks and meet specific goals. Good examples of AI implementations include Amazon’s Siri and Alexa voice-command devices and self-driving cars being developed by Google and Tesla.At K S, over the years we’ve implemented AI in our smart wire bonders to reduce human intervention in our ProCu-7, PSP-2, ProCu Loop 2, Pro Bump and overhang processes.Thanks to AI, with senses of signals from the bonder, we can reduce the amount of parameters that an engineer or technician have to do trial and error. With on bonder metrology, PBI, loop height, wire sway features, AI allows us to measure process efficiency and provide feedback.Over several years of AI development, we have leveraged the technology to monitor machines and provide real-time performance feedback in order to provide better closed loop control such as short tail recovery in our bonder process. We can also use the data to predict machine behavior, monitor its health and track maintenance. Ultimately, AI enables fabs to improve manufacturing efficiency, productivity, yields and device quality.Ng: What’s an example of how AI has solved your manufacturing equipment problems?Chong: We’ve used AI to set RPM (real time monitor) limits, identify defective P-parts and monitor various conditions such as wire size and capillaries. These types of cases can arise in any manufacturing environment as humans make process mistakes or use the wrong part for a machine. With AI, we can prevent these problems and reduce the risk of further material lost from the wire bonding process.Ng: What advice do you have for factories looking to implement smart manufacturing systems?Chong: To build a smart factory, start by focusing on a clear set of business objectives and how smart manufacturing will help minimize or eliminate current factory inefficiencies. In other words, start with the end in mind – the problems that needs to be solved and the business goals – and identify the information you need to demonstrate ROI. Do you need to resolve, automate or improve processes or just to be more efficient? Before investing millions or billions of dollars to build a smart factory, identify those clear goals upfront. Then map out the particulars of implementation to avoid major problems around standards, protocols and connectivity.Bee Bee Ng is president of SEMI Southeast Asia.
Read More
Semiconductor equipment spending is mounting a strong recovery on the strength of explosive chip demand for work-at-home and study-at-home electronics fueled by the COVID-19 pandemic. Despite the growth, the 2017-2018 memory boon that triggered a critical subsystems shortage is still fresh on the minds of equipment suppliers as they worry whether critical subsystem providers can keep pace with the rebounding chip industry while managing the fallout from the COVID-19 pandemic.Hideyuki Koishi, president of HORIBA STEC, Co., Ltd., a leading supplier of mass flow controllers (MFCs), one subsystem critical to semiconductor production, recently spoke with SEMI about the company’s response to the COVID-19 outbreak, the pandemic’s impact on the global supply chain and the company’s ability to meet the demand for MFCs. SEMI: What COVID-19 countermeasures has HORIBA STEC taken?Koishi: To ensure employee safety and security while maintaining a stable supply of products to our customers, we started to deploy company-wide countermeasures when the Japan government declared a nationwide state of emergency to curb COVID-19 infections on April 16.HORIBA STEC and the entire HORIBA group formed a global COVID-19 task force and centralized all local outbreak decision-making to drive a rapid and effective global response. We quickly implemented work-at-home practices for our office staff and provided a safe environment for our factory workers, who are essential to maintaining product supplies, by establishing social distancing protocols and restricting site visits to essential workers. We also distributed face masks to all employees and placed disinfectant dispensers near the door of every room so employees could wash their hands before entering.To help on-site employees follow our social distancing guidelines, we reduced seating at cafeterias and converted meeting rooms to offices to give employees ample work space. We also established invisible walls in manufacturing facilities with multiple collocated divisions to restrict workers to their assigned areas, a containment measure that helps with social distancing while minimizing the risk of an entire factory shutdown if a worker contracts the virus. SEMI: Have you experienced supply chain disruptions due to COVID-19 outbreak?Koishi: Even though our supply chain extends overseas and includes China, fortunately we have not experienced any significant disruptions thanks to the broad geographic distribution of our supply chain. In addition, because many of our critical components are sourced in Japan, pandemic-related impacts to our business have been limited.Long before the COVID-19 outbreak, we organized a community called Rakuraku-kai with our suppliers in Japan to build and maintain close relationships. Although the community name suggests it is exclusive to Kyoto-based suppliers, its reach is a nationwide. After the declaration of state of emergency in June, the supplier community gathered for an ad hoc meeting to exchange information and share perspectives on the COVID-19 crisis.SEMI: Did you have any pandemic protocols in place before the COVID-19 outbreak?Koishi: In 2014, HORIBA group launched Stained Glass, a project designed to increase workforce diversity at HORIBA group companies through initiatives such as placing more women in decision-making roles and encouraging working at home to help employees better balance job demands with their family lives. As part of Good Place, the project’s program to increase the work-at-home rate, HORIBA group deployed a web-based meeting system and encouraged workers to transition from physical to online meetings. Good Place has helped our IT team and workers smoothly implement our work-at-home practices.Working at home is a beneficial practice regardless of its effectiveness in curbing infections. Employees can reduce commute time, increasing their quality. And it’s much easier and more affordable for international participants to join meetings since they’re spared the time and cost of travel. This year HORIBA group also moved its three-day bi-annual global meeting online to make them safer and more economical. The meeting is attended by about 100 leaders of group companies and business units.SEMI: Do you have any concerns about meeting demand for mass flow controllers?Koishi: We doubled the capacity of our main mass flow controller factory in Kumamoto prefecture in 2018 and with more floor space available for further expansion, we see no major barriers to meeting the growing demand from international customers in 2021 and beyond. Nonetheless, we must sustain the best possible COVID-19 countermeasures to maintain production while ensuring the safety of our employees.SEMI: Are you make any social contributions to combat the virus?Koishi: Semiconductors are not only indispensable for the electronics behind remote work, education and healthcare but they also play a critical role in developing COVID-19 therapies and vaccines. Thus, at HORIBA STEC, we believe our most important contribution is to maintain steady a supply of our mass flow controllers and other key semiconductor equipment components.HORIBA group also participates in two important pandemic initiatives. The Open COVID-19 Declaration program calls on intellectual property owners to make their patent rights, utility model rights, design rights and copyrights freely available in the fight against COVID-19. The program’s sole purpose is to stop the spread of COVID-19. HORIBA is among the 20 founders1 of this initiative.In June, HORIBA joined a push by the National Institute of Advanced Industrial Science and Technology (AIST) to develop a simple and rapid COVID-19 antibody test chip system. We’re contributing our expertise in immunoassay analysis and clinical laboratory equipment to help develop the system. SEMI: What have you learned from the COVID-19 outbreak?Koishi: The COVID-19 crisis has posed unprecedented challenges. Everyone hopes to return to normal soon but in reality things will never be exactly the same as before the crisis.Japan might have lagged other countries in its use of IT to improve business efficiency, but as we deal with the new coronavirus, both companies and their employees have been tirelessly considering reforms to the way we work through digitalization. I believe it will be difficult for companies to survive in the new normal unless they can incorporate these types of changes into their operations.On the other hand, I've also been reminded of the importance of traditional, analog communication. While we conducted all of our hiring interviews online this year, face-to-face meetings are a much richer experience that gives the prospective employee and the hiring company a much better sense of each other. In addition, as a company we need to continue to improve our ability to supply products so we can overcome challenges like the pandemic. COVID-19 has taught us our change needs to be more robust. We also need to evolve our business continuity plan to extend well beyond countermeasures to natural disasters such as typhoons and earthquakes. What matters most is that we apply the lessons of COVID-19 to make our business more resilient.[1] Ajinomoto Co., Inc., Canon Inc., Chanel G.K., GenoConcierge Kyoto, Inc., Honda Motor Co., Ltd., Horiba, Ltd., Konica Minolta Inc., Kyoto University, LSI Medience Corporation, Mitsui Knoledge Industry Co., Ltd., NEC Solution Innovators, Ltd., Nikon Corporation, Nissan Motor Co., Ltd., Rohm Co., Ltd., SRL, Inc., Shimadzu Corporation, Teijin Limited., Toyota Motor Corporation, Tsubakimoto Chain Co., and Yahoo Japan Corporation.Yoichiro Ando is a marketing staff member at SEMI Japan.
Read More
Connectivity. Electrification. Shared Mobility. Autonomous Driving. McKinsey Company cites these four disruptive trends behind future mobility — dynamics that could help to transform quality of life for hundreds of millions of people.McKinsey Company predicts that by 2030, mobility innovation could dynamically alter everything from safety in human locomotion to air quality, public spaces and power systems. Much the same way that tiny plankton in our oceans sustain aquatic animals, MEMS and sensors, while small, are crucial building blocks of integrated mobility.As partner at McKinsey Company, Andreas Breiter will explore this connection during his MSEC 2020 presentation, Future Mobility Enabled by Sensorization. SEMI recently caught up with Breiter to preview his October 7 talk at SEMI’s first virtual MEMS Sensors Executive Congress, October 6-8 and 13-15, 2020.Register now for MSEC 2020 and explore this topic with Breiter during the live Q A portion of his presentation.SEMI: You play a dual role at McKinsey Company, advising clients in advanced industries on capital investments and serving on the leadership team of the McKinsey Center for Future Mobility (MCFM). What is the relationship between them?Breiter: Mobility has become so much more than the auto sector. Today when we say future mobility, we’re talking about the convergence of many exciting developments influencing the ways that people and goods move around. Cars have become computers, and we now have to contemplate new frontiers, such as air taxis and electric vehicle infrastructure.Mobility is changing so quickly that it’s inspiring decision-makers from other market sectors to explore what implications it will have for them. We’re helping mining companies think about their haulers, retailers think about their footprints, and insurance companies plan for autonomous vehicles. The MCFM exists as a global think tank to focus on these frontier topics, helping to ensure we are ready for the future. During my MSEC presentation, I’ll explore how those future topics are influencing automotive mobility in the short- and long-term. The MCFM is even more forward-looking, so we’re just starting to build scenarios for what might come in 2040 and beyond.SEMI: How are changes in the mobility ecosystem affecting the automotive value chain?Breiter: In the past, the automotive value chain was clearly structured. We had sensor companies selling to Tier 1 suppliers, who would in turn sell to OEMs, who would sell directly to end customers.The value chain has grown more complex, however. In the future, we might see fleets of robotaxis, which will be owned by companies instead of by individual consumers. Already today, rideshare companies are game-changers because consumers can travel by car without owning one.Plus we see companies offer parts of the user experience such as user interfaces for automotive infotainment. In the past, everything in the car was branded by the OEM, but now we have third-party platforms that let us control some of our automotive infotainment options.SEMI: How are MEMS and sensors suppliers participating in this new value chain?Breiter: The pervasive use of sensors in cars has driven automotive OEMs and Tier 1 suppliers to work directly with suppliers, whose close involvement eases the complexity of integration. Just think about the sensors used in autonomous driving. Getting that right is safety-critical.We’re also seeing suppliers go beyond the individual component level to provide complete systems-level solutions. Advanced driver-assistance systems (ADAS) are a good example.SEMI: Automotive applications tends to have some of the longest design-to-delivery cycles in industry. Will this ever change?Breiter: The automotive product lifecycle was typically five-plus years, with a few years of development before that and continued service after the end of the lifecycle. That gives MEMS and sensors suppliers a 10+ year timeline on one model.With so much innovation taking place, this slow cycle won’t work forever. Over-the-air (OTA) updates, for example, enable new features when they become ready for deployment. I expect we’ll see OTA updates from many end manufacturers in coming years. SEMI: What changes do you foresee in ADAS and autonomous driving?Breiter: ADAS and autonomous features will become much more common. We’ve already witnessed this progression, with introductions first in premier models and later rolling out in more affordable vehicles. Lane-change assist and rear camera followed this path and are now pretty standard. Collision avoidance, as a safety-critical feature, is likely next in line for more widespread adoption.As for fully autonomous driving, consumers will accept that only when it becomes safer than a human driving a car.SEMI: Where is the greatest opportunity in the next five years?Breiter: Electrification of vehicles is number one. When it comes to engines, we’re moving from internal combustion to hybrid and then to electric. Since OEMs are adding sensors for the battery system, for battery management, and for electric motors, this progression represents growth opportunity for sensors suppliers – in particular for hybrid vehicles that contain both powertrain technologies.But that’s not all when it comes to sensors. Outside of powertrains, new sensors are added to enable a variety of functions, including, for example, ADAS and autonomy, as well as increased interior content, such as mood lighting.SEMI: Is there anything surprising coming, sensor-wise, in mobility?Breiter: To enable intelligent traffic systems, you need to make infrastructure smarter — which brings us to sensors. We’re going to see roads and other assets in infrastructure sense the state of traffic, sense what traffic participants are doing, and support connectivity between, for example, the infrastructure, vehicles on the ground, pedestrians on walkways and drones in the air.SEMI: What would you like MSEC attendees to take away from your presentation?Breiter: We’re living in a transformative era for the mobility industry. During the last 100 years of mobility, the ecosystem barely changed. In recent years, however, we’ve seen massive technological gains, largely enabled by semiconductors, MEMS and sensors. Instead of serving as just one of many suppliers, I’d encourage MSEC attendees to anticipate future mobility challenges so they can offer solutions to OEMs and Tier 1 suppliers accordingly.For more information, visit McKinsey Center for Future Mobility. MEMS Sensors Industry Group® (MSIG), a SEMI technology community that connects the MEMS and sensors supply network in established and emerging markets, enables members to grow and prosper. Visit us today.Andreas Breiter leads McKinsey’s capital-investment work for advanced industries in North America as well as its Center for Future Mobility on the West Coast. In his advisory work, Breiter serves a broad range of companies in the automotive sector, including car and truck manufacturers and their suppliers, as well as companies in the utilities and renewables space. He helps executives make strategic choices around product development and helps companies stay ahead of emerging trends, such as autonomous driving, connectivity, electric vehicles, and shared mobility.Andreas holds a Ph.D. in Operations Management and studied in Germany, France, the U.S. and Canada.Nishita Rao is product marketing manager at SEMI.
Read More
At the 1964 New York World’s Fair, Walt Disney and his team of Imagineers debuted Audio-Animatronics® in four attractions, Great Moments with Mr. Lincoln, General Electric Carousel of Progress, Ford Magic Skyway, and it’s a small world. As “a new type of animation” that Walt said was “so lifelike that you might find it hard to believe,” Audio-Animatronics captivated audiences, setting the stage for the technological innovation that would transform theme-park attractions for decades to come. While the Audio-Animatronics in classic Disney® attractions such as Enchanted Tiki Room and Pirates of the Caribbean® continue to delight park-goers, more modern attractions take full advantage of the miniaturized, sensitive enabling hardware components, software algorithms, and connectivity technologies that are available to today’s engineers.When Michael Tschanz, director of engineering technology and analysis, a segment within Disney Parks, Experiences and Products’ Global Engineering and Technology department, gives the opening keynote at MSEC 2020, SEMI’s first virtual MEMS Sensors Executive Congress (October 6-8 and 13-15, 2020), attendees will get a rare look inside the magic of select Walt Disney World attractions. Join MEMS Sensors Industry Group and SEMI on October 6 for Tschanz’s keynote presentation, Model-Based Design and Scientific Data Analytics of Disney Attractions — and experience video footage that you won’t see anywhere else. Register now for MSEC 2020.MEMS Sensors Industry Group® (MSIG), a SEMI technology community that connects the MEMS and sensors supply network in established and emerging markets, enables members to grow and prosper. Visit us today.In his role at Disney, Michael Tschanz leads a multidiscipline team which develops detailed mathematical and physics models for transportation, ride and animatronic systems, custom software and network applications, and robotics. The responsibilities for this team also include the development of optimization algorithms, servo controllers, interactive/immersive experiences, data analytics, and material process solutions. Michael’s rich and diverse background includes designs of numerous attractions at various Disney theme parks including: Test Track® Attraction; Mission: SPACE® Attraction; Toy Story Mania!® Attraction and the Expedition Everest® Attraction. Michael also designed all the velocity profiles at the worldwide locations of The Twilight Zone Tower of Terror™.Nishita Rao is product marketing manager at SEMI.
Read More
MEMS sensors have come a long way over the past few decades. The late 1990’s brought us the mass production of both MEMS accelerometers for automotive air bag crash sensors and MEMS gyros for rollover detection and anti-locking braking systems (ABS). In the early 2000’s, MEMS sensors made the jump from automotive to mobile and consumer electronics, first with a MEMS microphone in the wildly successful Motorola RAZR phone and then with a MEMS accelerometer in the first Nintendo Wii remote.Following this initial period of MEMS’ commercialization, the timetable for the mass proliferation of both MEMS and non-MEMS sensors accelerated dramatically. Just take Apple iPhone. Released in 2007, the first iPhone had one MEMS accelerometer and one proximity sensor. Released 10 years later, iPhone X included four MEMS microphones, a barometer, three-axis gyro, MEMS accelerometer and proximity sensor, an ambient light sensor and an infrared (IR) sensor, a magnetometer, and multiple image sensors. For perspective’s sake, well over two billion iPhones have been sold since 2007, making iPhone a major growth-driver in MEMS. According to Yole Développement[i] (Yole), MEMS will generate $10.9 billion in revenue in 2020 alone (non-MEMS sensor revenue will be even higher), spanning automotive, consumer and mobile, Internet of Things (IoT), medical and healthcare, aerospace, industrial and other markets.With so much growth behind us, what’s ahead? Jens Fabrowsky, executive vice president of Automotive Electronics at Robert Bosch GmbH, will share his insights on the future of MEMS during his MSEC 2020 keynote, The Next 10 Years of MEMS: An Outlook on Opportunities and Challenges. I recently spoke with Fabrowsky to preview his October 15 presentation at SEMI’s first virtual MEMS Sensors Executive Congress, October 6-8 and 13-15, 2020. Register now for MSEC 2020 and explore this topic with Fabrowsky by participating in the Q A segment of his presentation.SEMI: What are some of the primary challenges facing the MEMS industry?Fabrowsky: Development costs for new generations of MEMS sensors are increasing, leading to several major shifts. To compensate for rising development costs and reduce risk, MEMS sensors suppliers are pursuing wider, diverse markets instead of just targeting high-volume applications. At the same time, end-device manufacturers are demanding greater product differentiation, but they don’t want to pay a premium for it or wait for new hardware iterations. To stay competitive, sensor suppliers are providing software solutions that support new features and functionality. That approach is more cost-effective and speeds design-to-production cycles. SEMI: What factors are increasing development costs for new MEMS sensors, and what can companies do to mitigate their R D risk? Fabrowsky: As with most electronic components, MEMS’ costs are driven by development and capital expenditures. The increasing complexity of the content, especially in interface ASICs and software, makes MEMS development a multidisciplinary feat, requiring several competencies across multiple design centers to meet ever-demanding timelines.Manufacturing also plays a role. We often see dedicated manufacturing lines built for new MEMS products, which stresses both investments and capacity planning. Working together as an industry, we can reduce risk and costs by applying the same manufacturing process to more than one generation of product, which will speed time to market, increase volumes and improve ROI. SEMI: To what degree will the COVID-19 pandemic continue to affect sensors suppliers?Fabrowsky: MEMS manufacturing flows have been affected by disruptions in the supply chain. While the benefits of multiple sourcing and more direct ownership of the flow itself (on-shoring, vertical integration) have helped us, no one in the industry can claim they are out of danger, especially if a new wave of contagion occurs. Our industry relies heavily on just-in-time manufacturing and logistics, and we are all watching for influences that could alter flow. The pandemic has reminded us all that an important competitive advantage is a predictable, secure supply — which also comes at a cost that the end customer must value. SEMI: Why and how are traditional hardware companies like Robert Bosch differentiating their platforms for end-device manufacturers? Fabrowsky: On-shoring was already a trend before the pandemic. We’ve always believed in and are still investing in our own manufacturing facilities. That includes the 12-inch ASIC fab in Dresden, Germany, where we expect to manufacture future generations of power and control electronics to satisfy the growing appetite for silicon that vehicle electrification demands.We think that one of our biggest differentiators is that our portfolio includes more than just components: Close collaboration with our internal partner divisions gives us comprehensive system know-how across the automotive supply chain. On the consumer-electronics side, we have extensive partnerships with makers of application processors, wireless systems, and sensor processing software. With this expertise behind us, we can provide flexible system-integration options to our end customers — who also benefit from a mature supply chain that supports high volumes and field-tested quality.SEMI: What does customer demand for software solutions mean for sensor suppliers and how will suppliers evolve to meet this need? Fabrowsky: In some silicon product business units, the R D effort to develop software is higher than the effort to design the hardware! Software is not only what’s needed on the application layer. It also runs the interface to the processors – the drivers. In addition, increasingly complex testing software ensures high yield and minimizes defects. On the application layer, we are increasingly using and promoting open-source platforms to encourage better collaboration throughout the ecosystem. In contrast, companies that charge fees to access their own proprietary software environments are missing the opportunity to remain competitive in the long run. SEMI: Why are end-device manufacturers looking for plug-and-play solutions instead of standalone devices? Fabrowsky: Consumers of electronic devices always want products with more features and lower prices. Their requirements produce a trickle-down effect that reaches all the way to component suppliers such as ourselves. This requires us to manage a healthy innovation pipeline, and to choose products and technologies that promise growth and high volumes. This isn’t always simple, however, and many times the component itself is not enough. Think of our Light Drive projector for Bosch Smartglasses. The only way we can hope to win designs in this market is by realizing a fully integrated module, with our own scanning mirrors and driver chips, as well as our integration of laser modules and the display system. This lets us offer an individually tested and calibrated end product ready for assembly.SEMI: What would you like MSEC 2020 attendees to take away from your presentation?Fabrowsky: We’ll be looking at what’s driving the next decade of MEMS applications. For example, the embedded computing inside the sensors, together with enhancements in integration, materials and packaging, will increase the pervasiveness of MEMS sensors and actuators as touchpoints between electronics and the physical world. This will create a new form of intimacy between us and the machines, which we call Artificial Empathy.To learn more about Bosch Smartglasses Light Drive and other MEMS advancements, register now for MSEC 2020.Robert Bosch GmbH is a longtime member of MEMS Sensors Industry Group® (MSIG), a SEMI technology community that connects the MEMS and sensors supply network in established and emerging markets, enabling members to grow and prosper. Visit us today.Jens Fabrowsky began his more than 20-year career at Bosch Group as department head responsible for hydraulic units in the Blaichach plant, Germany Chassis Systems division, in 1999. He soon moved onto technical plant manager and later to plant manager within the company’s Germany Gasoline systems division. He has held the role of executive vice president, Automotive Electronics at Robert Bosch GmbH, since April 2012. Fabrowsky studied mechanical engineering and industrial engineering at the University of Stuttgart (Germany) and the Technical University of Munich (Germany). [i] Status of the MEMS Industry report, Yole Développement, 2020.Nishita Rao is product marketing manager at SEMI.
Read More
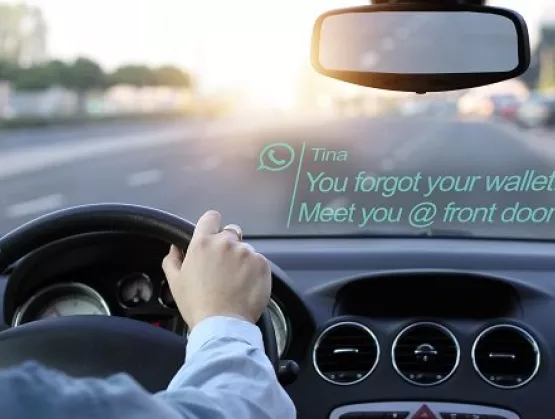
Jack McCauley understands the interplay between video game hardware and human interaction like few others in the industry. He designed the guitar and drums for Red Octane’s (later Activision’s) Guitar Hero video game series. As co-founder and chief engineer of Oculus VR, he designed the Oculus DK1 and DK2 virtual reality (VR) headsets and helped guide the company through its acquisition by Facebook in 2014. Now active in automotive technology, he builds cars at Black Lab, his private R D facility and hardware incubator in Livermore, California. And, in no small feat, he thinks he’s solved the head-tracking problems in augmented reality (AR)/VR headsets – which he’ll demonstrate during his keynote presentation, MEMS Applications in Augmented Reality, October 6 at MSEC 2020. SEMI’s first virtual MEMS Sensors Executive Congress. The event is October 6-8 and 13-15, 2020, and registration is open. I interviewed McCauley to preview his presentation. Register now for MSEC 2020.SEMI: What inspired you to become the first person to use a MEMS sensor in a gaming device?McCauley: When I started designing the Guitar Hero peripherals, I had intermittent problems with the motion tracking. I switched to a Freescale single-axis accelerometer, developed some IP around it, and that fixed the problem. That’s how I became an early customer of MEMS. SEMI: When you pioneered immersive VR gaming experiences at Oculus VR, tech industry analysts predicted widespread adoption of VR for gaming. What do you think happened?McCauley: There are a lot of reasons why VR hasn’t become the standard bearer for gaming. Gaming used to be a solitary activity, but as companies like Microsoft and Sony got behind multiplayer gaming, we realized many gamers found the social aspect more important than the visual aspect. Many gamers are content to play on a 2D screen or on multiple monitors because they’re playing against many people. The proliferation of internet connections worldwide has also promoted the kinship and social aspect of gaming.SEMI: Do you think VR has a place in other applications?McCauley: I think it has a lot of potential in real estate, VR movies, and engineering and design, among other areas. The automotive designer Henrik Fisker, for example, created whole vehicles in a game-engine model. If you wanted to buy one of his cars, let’s say, you could change the color and upholstery, for example, and then view it in a VR environment. SEMI: One of the biggest obstacles to VR adoption is the motion sickness some people experience during game play. What would you do to fix that?McCauley: The vestibular system in the brain, which uses the inner ear, is crucial to helping you balance. If there’s a mismatch between what your eyes see and your brain is perceiving, you’re likely to feel dizzy. I’ve built a VR headset that uses a MEMS pico projector with micromirrors and a small laser for position tracking as well as for facial tracking and modeling. But the platform’s not for sale.Still, many of the technical advances that we’ve made in VR are helping us with AR development. The increasing power of mobile chipsets and GPUs, the decreasing geometry for individual transistors and the way specific chips are processed, screen interfaces that will drive a 4K panel at a high frame rate, plus MEMS devices inside the eyewear for rotations and tracking are all helpful innovations.SEMI: When designing cars in your own lab, you’re doing a lot of work with AR. What do you think of AR’s commercial viability?McCauley: I know there are well-funded AR programs in place at major companies. That’s because mobile-device companies want an omnipresent phone in front of your face. I thought Google Glass, for example, was brilliant, but it was way too early for that product, and there was too much hype behind it.McCauley's latest R D project is a vehicle that incorporates augmented features and a computerized display. The vehicle is a custom built, environmentally friendly super-car with enhanced driver safety and high vehicle performance. AR is appealing because it lets people see through a screen – and have objects appear on that screen – while they are moving through space. My son actually came up with one of the ideas I’m implementing in a car I’m designing. We were driving in Spain, and he suggested that instead of using Google Maps to show me driving directions – which would force me to look down at an infotainment display – a sign could appear on AR glasses that would instruct me how to drive to Italy. That’s just an example of how we’ll use AR. SEMI: After you sold Oculus VR to Facebook, you began investing time and resources into engineering education. Why did you make that choice?McCauley: I’m originally from a blue-collar family, and then I got an education at Berkeley. That made a major difference in my life. When I sold Oculus, I donated to education-focused charities primarily, because an education can lift an entire family out of poverty. Let’s say your family are farm workers, but you get a degree in engineering and land a job at Apple. That could produce a ripple effect. As other members of your family and people in your community see the benefits of your education, they’re more likely to get an education, too. SEMI: What would you like MSEC attendees to take away from your presentation?McCauley: I appreciate what the MEMS industry has done for VR because if Oculus didn’t have a nine degrees of freedom (9DoF) IMU, no one would have bought our company. A new application will come along sooner or later that will require a different type of MEMS technology, and I have total confidence that the MEMS industry will deliver what’s needed. For more information on McCauley’s R D projects or on his position as Innovator in Residence at UC Berkeley’s Jacobs Institute for Design Innovation, visit his website. MEMS Sensors Industry Group® (MSIG), a SEMI technology community that connects the MEMS and sensors supply network in established and emerging markets, enables members to grow and prosper. Visit us today.Jack McCauley is an Innovator in Residence at the Jacobs Institute for Design Innovation, where he mentors students, lectures in courses focused on product design and design for manufacturing, and leads research and development projects focused on applications of augmented, virtual, and mixed reality for design professionals and students.McCauley graduated from Berkeley Engineering with a B.S. in Electrical Engineering and Computer Science in 1986, and credits the time he spent at Berkeley as an undergraduate with helping to ignite his career. Maria Vetrano is a public relations consultant at SEMI.
Read More
The costs of production are typically based on labor and materials and define manufacturing expenses. But is this approach accurate enough? What about the cost of poor quality and lack of efficiency in production? How is the pandemic impacting semiconductor manufacturing and what can we expect from the future?SEMI recently spoke with Dr. Eyal Kaufman, founder and CEO of QualityLine, a Kiryat Gat, Israel-based provider of smart manufacturing analytics solution, about manufacturing controls and how to select the best data source to improve product quality and yield. Kaufmann provided a snapshot of current best practices used by the company to improve manufacturing efficiencies and product quality while reducing costs. He also discussed the COVID-19 pandemic’s impact on semiconductor smart manufacturing and how artificial intelligence (AI) can help keep factory workers safe.For additional insights on smart manufacturing, join the virtual SEMI Global Smart Manufacturing Conference, October 20 - 22, 2020. Registration is open.SEMI: Real manufacturing costs are calculated based on different aspects such as failures in production, repairs, products returned, scrap of components or late deliveries. Lack of quality and efficiency in manufacturing can undermine a business. How are you helping businesses overcome these challenges?Kaufman: To increase profit margins, it is essential to identify inefficiencies and what improvements to prioritize. Once manufacturing quality and efficiency deficiencies have been measured, the next step is to continuously collect manufacturing data in order to run the final cost analysis and use the analytics to improve the manufacturing process.Smart manufacturing makes it possible to detect anomalies in automated factories, improve production performance and increase profitability. Today, automated data are collected from every machine and piece of test equipment in the factory. Still, manufacturing data collection in many industries remains manual and expensive because of the time and human resources involved. A real-time analytics system can automatically collect all data sources and select the relevant data for analysis, which today is the most accurate and effective way of measuring and resolving quality and efficiency deficiencies.Data-driven decisions made by smart manufacturing reduce costs and improve manufacturing strategies, enabling factory operators to increase product quality, drive higher production capacity and enhance product design for manufacturability. Analytics solutions monitor shop floor operations accessing vendors and subcontractors’ products criterion to run root cause analysis. All those data will reduce the return rate of faulty products and accelerate return on investment. This is why we definitely need smart manufacturing technologies!SEMI: Data accumulated during the manufacturing process includes vital information about failures, anomalies and machine usability. What data are necessary to create the best analytics solution?Kaufman: Many companies today run data mapping and automatic creation of data capture. They often wonder if they need to use testing data, sensors data or product design data, or whether they should collect feedback from their customers and vendors. The best way to create an effective manufacturing analytics system is to use data sources such as: Feedback from customers (returned units, customers complaints, etc..) Testing data from automated test equipment and manual test activities Feedback from technicians repairing faulty units Analysis of testing processes done by vendors Sensors data Data from our ERP/MES systems Artificial intelligence enables any type and size of data structure, even accumulated data, to be automatically integrated and interpreted. AI-based analytics can also establish correlations between each manufacturing stage to help factory operators quickly conduct deep diagnostic and root cause analysis for problem solving and prevention – all while leaving intact a factory’s existing process, machinery and data output. Machine learning evaluates how a factory runs its database and puts all the information generated into an analytics solution that provides the know-how to continuously improve factory efficiency.SEMI: How do you select the best data source to improve manufacturing quality and yield? Kaufman: The accuracy and integrity of data accumulated in our manufacturing process is key to controlling and improving yield and quality while reducing manufacturing costs. Smart manufacturing is a technology-driven approach that uses digital and remote connected machinery to monitor the production process. The goal is to identify anomalies in manufacturing processes and leverage analytics to improve process yield and product quality.To select the relevant data, we collect each type and source of data that can improve the efficiency of a real manufacturing cell: Test data from Automated Testing Equipment Test data from Manual Testing Processes Analyses of repairing processes (failed units during the manufacturing process and units that were returned from customers) Once the data structure is collected, the next step is to turn it into actionable information in the manufacturing process. QualityLine smart manufacturing solutions provide a complete one-stop solution to interpret any manufacturing data structure. Our advanced manufacturing analytics solution detects quality and yield anomalies to reveal production line inefficiencies and opportunities to improve manufacturing quality and efficiency.SEMI: How would you describe your approach?Kaufman: Industry 4.0 in manufacturing claims to be the fourth generation of the industrial revolution. Advanced technologies like manufacturing intelligence and machine learning can efficiently achieve zero defects on manufacturing lines. Digital factories leverage technologies and methodologies including: Big data Self-optimization Self-configuration Self-diagnosis Cognitive and machine learning Smart manufacturing technologies enhance the manufacturing process by continuously collecting and analyzing data in real-time to achieve and maintain high quality performance. The goal is to achieve a significant increase in efficiency and yield while reducing waste and inefficiency.Until now, there has been no viable way to integrate all saved manufacturing data into a unified database. QualityLine advanced manufacturing analytics make it possible for any factory to become digital without installing new hardware, which can be expensive and require not only the extensive integration of existing data but investments in training. Our user-friendly solution integrates manufacturing data for industries with zero automation by first collecting and analyzing data from any type of manual test procedure and then integrated it into manufacturing analytics to improve efficiency.SEMI: Why are Pass/Fail criteria insufficient for controlling manufacturing yield and quality?Kaufman: Managing a mass manufacturing process is always a challenge because hundreds of tasks must be successfully completed before products can ship to customers. At QualityLine, we establish a test process for each stage of the production flow, from the incoming raw material to the final stage prior to the delivery of finished goods to the client. To prevent unexpected downtime incidents, waste and defective products, we collect and interpret every type of relevant data and turn it into meaningful information, setting up the following capabilities: Collection and interpretation of test and process data of each single unit and from each process and plant Automatic detection of quality and yield problems Accurate and quick root cause analysis process Automatic alerts to abnormal issues Prediction process potential and level of failures Measurement of key performance indicators Many manufacturers base their test criteria of each parameter on one key indicator – Pass or Fail. If the test result shows a Pass, then the unit is ready to move on to the next manufacturing stage. If the test result shows Fail, then the unit is sent to a technician for further analysis.A simple Pass or Fail criteria for product quality is far from sufficient since it provides little or no information about edge cases, where one or more of the technical parameters of the unit under test is only within its allowed tolerance. Edge cases may lead to unit failure during operation such as in extreme environments (cold, heat, humidity, electrical overload, impact, etc.). In fact, when running a mass manufacturing line, it is impossible to continuously digest all the detailed information collected from testing stations. Data is analyzed in detail only when a critical quality problem emerges and further analysis is required to understand the root cause.Information overload and the disregard of important parameters makes it hard to control the process and improve quality and yield. New technologies make fast and scalable data integration possible so data can be collected in real time to detect quality issues early, identify complex process disruptions to avoid delivery delays and ensure the best possible product for customers. Only by accurately analyzing data as actionable information can factory operators control the manufacturing quality process.SEMI: How has COVID-19 impacted the smart manufacturing market? How has your technology helped factories remain online?Kaufman: Smart manufacturing is playing a significant role by helping manufacturers overcome COVID-19 challenges such as workforce reductions, social distancing, drops in sales for some specific products and extreme pressure to cut operational costs.Manufacturing leaders turned to us for a solution to the challenges of maintaining efficient factory operations with a limited workforce and reduced number of operating hours. Filling factory orders with fewer people on the floor is a struggle. Digital factory technologies enable remote monitoring of operations to increase efficiency and capacity. We are helping our clients improve efficiency while reducing costs. Our remote monitoring technology can provide the operational visibility to floor managers and engineering teams who cannot go physically to the factories due to safety restrictions. With our advanced manufacturing analytics, they have full end-to-end visibility and can remotely diagnose and solve production line issues. During this critical time, we are proud to be improving remote monitoring solutions to help the industry withstand the pandemic. Some of our clients would have closed their factories otherwise. We’ve been working to integrate manufacturing data in factories that were previously unautomated to drive high automation levels. Integrating processes with existing factory data, regardless of customer’s protocols or automation level, is our great technology advantage.SEMI: How will manufacturing and its supply chains look after COVID-19?Kaufman: Smart manufacturing is currently a necessity. We collect and analyze data not only to improve quality but to reduce client returns of faulty products by 50% and reduce waste by 22%, both critical points. Manufacturing challenges will continue to accelerate advancements in technology and improve efficiency, safety and productivity as more factory operators incorporate real-time data analytics and artificial intelligence (AI). SEMI: Will suppliers continue to explore new avenues for smart manufacturing technologies and what are their growth opportunities?Kaufman: Yes, definitely. The sector has already changed, with COVID-19 bringing both opportunities and challenges. Industry leaders are facing new pressure, with sudden materials shortages, drops in demand and worker unavailability. The growth opportunities for manufacturing are likely to be digital, as already evident in the immediate response to the crisis. Industry 4.0 solutions will be crucial to increase end-to-end supply-chain transparency, automation and data integration. QualityLine manufacturing analytics have improved key manufacturing performance metrics. For example, based on customer feedback, we’ve increased production yield by 30%, saving some of our customers millions of dollars. Improvements like this can help suppliers withstand pandemics.Dr. Eyal Kaufman, Founder and CEO at QualityLine, has senior management experience and over 25 years of expertise in business development, marketing, finance, operations, engineering and quality management at leading industrial companies. Prior to QualityLine, he served as VP of Mobileye, Cardo Systems, and Medisim Ltd., as well as CEO of OnTheGo Systems. Eyal holds a Ph.D. from California Intercontinental University, an MBA from City University of New York and a BSc. from the Technion in Israel.The SEMI SMART Manufacturing Initiative is a global effort to promote awareness and interest about smart manufacturing with focus on delivering industry-recognized best-in-class programs and services to enable members to maximize product quality, productivity and cost improvements through smart manufacturing. Activities are focused on building out core capabilities to enable smart manufacturing across the microelectronics supply chain.MADEin4 is a consortium of 47 partners from 10 countries connecting the full range of supply chain: from semiconductor equipment manufacturers and system-integrating metrology companies to RTOS and key applications such as the automotive industry. The MADEin4 Project develops next generation metrology tools, machine learning methods and applications in support of Industry 4.0 high volume manufacturing in the semiconductor manufacturing industry.Serena Brischetto is a senior manager of marketing and communications at SEMI Europe.
Read More