downloadGroupGroupnoun_press release_995423_000000 copyGroupnoun_Feed_96767_000000Group 19noun_pictures_1817522_000000Member company iconResource item iconStore item iconGroup 19Group 19noun_Photo_2085192_000000 Copynoun_presentation_2096081_000000Group 19Group Copy 7noun_webinar_692730_000000Path
Skip to main content
Default Banner Image

Technology and Trends

That FD-SOI can be a key to achieving near-threshold voltage design was an important point made during a #55 DAC expert panel. Entitled How Close to Threshold-Voltage Design Can We Go Without Getting our Fingers Burnt? the session was organized by Jan Willis of Calibre Consulting. Turnout was excellent. Btw, Jan (herself an EDA expert) was one of the original advisors in the formation of the SOI Consortium, and while this DAC panel was not meant to be about FD-SOI, it turned out be a focal point. Near-threshold voltage design* is an especially hot topic for IoT and edge-computing designers, for whom balancing performance, reliability and extremely low power is generally challenge #1. For them, the ability to get chips working at very low voltages translates into battery life savings. The original goal of the panel was “...to explore how far below nominal voltage we can design, in what applications it makes sense and in what ways it will cost us.” The description in the #55 DAC program noted that “Energy consumption is the driving design parameter for many systems that must meet 'always-on' market requirements and in IoT in general. For decades, the semiconductor industry has attempted to leverage the essential principle that lowering voltage is the quickest, biggest way to reduce energy for a SoC. Some today contend sub-threshold voltage design is viable while others argue for near-threshold voltage design as the minimum.” (Update 2 August 2018: a complete video of this panel is now available on YouTube -- click here to view it.) [caption id="attachment_12035" align="alignnone" width="958"] #55 DAC Expert Panel: How Close to Threshold-Voltage Design Can We Go Without Getting our Fingers Burnt? Left to right: Brian Fuller, Arm (moderator); Scott Hanson, Ambiq Micro; Lauri Koskinen, Minima Processor; Mahbub Rashed, GlobalFoundries; Paul Wells, sureCore. (Organized by Jan Willis of Calibre Consulting)[/caption] The panelists included: Scott Hanson - Ambiq Micro Mahbub Rashed - GLOBALFOUNDRIES Lauri Koskinen - Minima Processor Paul Wells - sureCore Ltd., Sheffield Brian Fuller of Arm served as moderator. [caption id="attachment_12033" align="alignright" width="200"] Panel organizer Jan Willis, Calibre Consulting[/caption] Following the panel Jan published the following excellent recap on LinkedIn. She graciously agreed for it to be reprinted here in ASN, for which we thank her. So without further ado, read on! #55DAC Expert Panel on Near-Threshold Voltage Sees Growing Opportunity Despite ChallengesFirst published on LinkedIn, June 27, 2018 by Jan Willis, Strategic Partnerships Marketing Executive Brian Fuller, Arm, skillfully guided a group of experts through the challenges of near-threshold design to conclude that the adoption is going to start gathering pace in a panel session at the 55th DAC in San Francisco on Monday, June 25. Scott Hanson, CTO of Ambiq Micro, led off by saying the list of what's not challenging is a much shorter list but that by taking an adaptive approach, they have been successful. It's required innovating throughout the design process including test where Scott said they had create their own "secret sauce" to make it work. Later on in the panel, Scott described designers in near-threshold as "picojoule fanatics" to overcome the limitations in design tools which are geared towards achieving performance goals. Lauri Koskinen, CTO of Minima Processor, agreed that adaptivity is key. Minima says it has to be done in situ in the design to make it robust for manufacturing while useful across more than one design. Later in the panel, Lauri indicated that FD-SOI is like having another knob available for optimizing energy in the Minima approach to near-threshold design. Mahbub Rashed, head of Design and Technology Co-Optimization at GlobalFoundries, highlighted the need for more collaboration between EDA, IP, and foundries to support near-threshold design but noted a lot of progress has been made on FD-SOI processes. Mahbub cited models down to 0.4V for FD-SOI processes are available now and GlobalFoundries is able to guarantee yield. Paul Wells, CEO of sureCore, validated that sureCore has bench marked their memories on GlobalFoundries FD-SOI with success. He reflected that FD-SOI has rapidly established itself as cost effective for a number of emerging markets. The panel all agreed that achieving quality on the memory at near-threshold voltage was much tougher than for digital IP. [Editor's note: sureCore's CTO wrote an excellent summary of their SRAM IP for FD-SOI in ASN back in 2016 – you can still read it here.] Paul went on to summarize at the end of the panel that near-threshold voltage is the way of the future and that it's gathering pace. Mahbub called upon the EDA community to step up to improve the tools for low energy design. Lauri and Scott both summarized that there were drivers emerging that will grow the addressable market for near-threshold voltage design. Lauri pointed to growth coming from the applications that require edge computing which he thinks will require near-threshold voltage design. Scott concluded the panel by pointing out that there's been a tremendous increase in performance of near-threshold voltage designs which will increase the addressable available market in the future. ~ ~ ~ This piece was first published by Jan Willis on LinkedIn, June 27, 2018. Here is the original. * As explained by Rich Collins of Synopsys in the TechDesign Forum: "Operating at near-threshold or sub-threshold voltages reduces static and dynamic power consumption, at the cost of design complexity. [...] A transistor’s threshold voltage (Vth) is the voltage at which the transistor turns on. Most transistor circuits use a supply voltage substantially greater than the threshold voltage, so that the point at which the transistors turn on is not affected by supply variations or noise. [...] In sub-threshold operation, the supply voltage is well below the Vth of the transistors. In this region, the transistors are partially On, but are never fully turned. Near-threshold operation happens between the sub-threshold region and the transistor threshold voltage Vth, or around 400 – 700mV for today’s processes.
Read More
Leti and Soitec have announced a new collaboration and five-year partnership agreement to drive the R D of advanced engineered substrates, including SOI and beyond. This agreement brings the traditional Leti-Soitec partnership to a whole new dimension and includes the launch of a world-class prototyping hub associating equipment partners to pioneer with new materials, The Substrate Innovation Center will feature access to shared Leti-Soitec expertise around a focused pilot line. Key benefits for partners include access to early exploratory sampling and prototyping, collaborative analysis, and early learning at the substrate level, eventually leading to streamlined product viability and roadmap planning at the system level. [caption id="attachment_12066" align="aligncenter" width="644"] CEOs Emmanuel Sabonnadière (Leti) and Paul Boudre (Soitec) announcing the new Substrate Innovation Center during Semicon West '18. (Image courtesy: Leti)[/caption] Leading chip makers and foundries worldwide use Soitec products to manufacture chips for consumer applications targeting performance, connectivity, and efficiency with extremely low energy consumption. Applications include smart phones, data centers, automotive, imagers, and medical and industrial equipment, but this list is always growing, along with the need for flexibility to explore new applications starting at the substrate level. At the Substrate Innovation Center, located on Leti’s campus, Leti and Soitec engineers will explore and develop innovative substrate features, expanding to new fields and applications with a special focus on 4G/5G connectivity, artificial intelligence, sensors and display, automotive, photonics, and edge computing. “Material innovation and substrate engineering make entire new horizons possible. The Substrate Innovation Center will unleash the power of substrate R D collaboration beyond the typical product road maps, beyond the typical constraints,” said Paul Boudre, Soitec CEO. “The Substrate Innovation Center is a one-of-a-kind opportunity open to all industry partners within the semiconductor value chain.” Whereas a typical manufacturing facility has limited flexibility to try new solutions and cannot afford to take risks with prototyping, the mission of the Substrate Innovation Center is to become the world’s preferred hub for evaluating and designing engineered substrate solutions to address the future needs of the industry, inclusive of all the key players, from compound suppliers to product designers. Using state of the art, quality-controlled clean room facilities, and the latest industry-grade equipment and materials, Leti and Soitec engineers will conduct testing and evaluation at all levels of advanced substrate R D. “Leti and Soitec’s collaboration on SOI and differentiated materials, which extends back to Soitec’s launch in 1992, has produced innovative technologies that are vital to a wide range of consumer and industrial products and components,” said Emmanuel Sabonnadière, Leti CEO. “This new common hub at Leti’s campus marks the next step in this ongoing partnership. By jointly working with foundries, fabless, and system companies, we provide our partners with a strong edge for their future products."
Read More
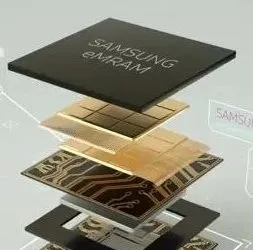
Per Arm, the industry's first eMRAM compiler IP is now on Samsung's 28nm FD-SOI technology. The announcement was made in a post by Kelvin Low, VP Marketing for ARM's Physical Design Group (read it here). He said that ARM has successfully completed their first eMRAM IP test chip tapeout. The Arm eMRAM compiler IP will be available from 4Q 2018 for lead partners. Samsung Foundry’s 28nm FD-SOI process technology is called 28FDS. eMRAM (which stands for embedded MagnetoResistive RAM) is a novel non-volatile memory (NVM) option positioned to replace incumbent NVM eFLASH, which has hit its limits in terms of speed, power, and scalability. Arm's new eMRAM compiler IP gives Samsung's 28FDS customers the flexibility to scale their memory needs based on the complexity of various use-cases, explains Low. “What drives the cost-effectiveness of this compiler IP is that eMRAM can be integrated with as few as three additional masks, while eFlash requires greater than 12 additional masks at 40nm and below,” he says. “Also, the eMRAM compiler can generate instances to replace Flash, Electrically Erasable Programmable Read-Only Memory (EEPROM) and slow SRAM/data buffer memories with a single non-volatile fast memory – particularly suited for cost- and power- sensitive IoT applications.” [caption id="attachment_11972" align="alignleft" width="300"] A key slide shown by Arm at the 2017 SOI Consortium's Silicon Valley Symposium (Courtesy: Arm and the SOI Consortium)[/caption] At the SOI Consortium's 2017 Silicon Valley Symposium, Arm said that they were stepping up their support of FD-SOI (read about that here) – and clearly they are! At that event, Arm VP Ron Moore gave a great presentation, which is freely available on our website: Low Power IP: Essential Ingredients for IoT Opportunities. Samsung, btw, has been offering 28FDS for about three years now. (ASN did a 3-part interview with Kelvin Low back in 2015 when he was a senior director of marketing for Samsung Foundry. It's still a useful read – you can get it here.) As of last fall, Samsung said it had taped out more than 40 products for various customers. And at the SOI Consortium's 2018 Silicon Valley Symposium, Hong Hoa, SVP said they'd already taped out another 20 this year (read about that here). https://youtu.be/EB14K8Gq5-w Samsung says the write speed of their eMRAM is 1000x faster than eFlash. They actually announced the industry's first eMRAM testchip tape-out milestone on 28FDS in September 2017 (you can read the press release here). They also did an eMRAM test chip with NXP. (BTW, Samsung has a really nice video explaining their eMRAM offering – you can see it above or on YouTube here.) As noted in ASN's Silicon Valley 2018 symposium coverage, the basic PDK for the Samsung 18nm FD-SOI process (18FDS) will be available in September 2018, with full production slated for fall of 2019. It will deliver a 24% increase in performance, a 38% decrease in power, and a 35% decrease in area for logic. RF for the 18FDS platform will be ready by the end of this year, and eMRAM beginning in 2019.
Read More
Dolphin Integration, a partner in the ENIAC THINGS2DO European FD-SOI project, showcased its achievements with PowerStudio™ during the project final review. Power Studio is Dolphin's cutting-edge EDA tool for safe Power Regulation Networks implementation. THINGS2DO, which stands for THIN but Great Silicon to Design Objects, was a 4-year, €120 million EU project (85% industry-funded) with over 40 partners that just finished up at the end of 2017. The goal was to build a design development ecosystem for FD-SOI. The project funded and supported the development of major FD SOI-based IPs and ASICs as well as EDA tools. (Another recent THINGS2DO announcement was Dream Chips’ ADAS SoC fabbed in GlobalFoundries’ 22FDX technology -- read about that here.) “Being involved in the THINGS2DO project was an opportunity for Dolphin Integration to start introducing FD-SOI in its automatic design methodologies,” said Frederic Poullet, Dolphin Integration’s CTO (read the press release here). “Dolphin Integration plans to offer a full suite of tools allowing its customers to implement right-on-first-pass Power Regulation Networks.” The company notes that THINGS2DO also proved that low power consumption makes FD-SOI a perfect fit for IoT and automotive applications. For instance, dynamic control of threshold voltage can be used to compensate for temperature variations, and to drive speed improvements by 200% in ultra-low voltage applications. Dolphin Integration provides energy efficient IPs and ASIC services dedicated to the low-power application market and supports its internal teams with tailor-made software tools. To address the specific needs of its customers in low-power design, Dolphin developed PowerStudio™, a global solution for the optimization of Power Regulation Networks (PRNet) to be used at an early stage of the SoC design process. In particular, it addresses new design challenges in noise and power supply integrity. The first module of PowerStudio™ will also embed architecture optimization features at the schematic level, in terms of FoM-based cost optimization, mode management, margin cuts and integrability rate-based risk optimization. Btw, Dolphin Integration Director Frederic Renoux gave an excellent great presentation at an SOI Consortium event in Nanjing, China last year, entitled Embedding power regulation activity control networks for best SoC PPA. Dolphin Integration joined Global foundries’ FDXcelerator™ Program last year (read the press release here) to streamline design in 22FDX®. "Our comprehensive and robust library of voltage regulators, power gating cells and logic modules, enables to deal cost-effectively and securely with power distribution, power gating, power monitoring and power control of any SoC design in 22FDX," Michel Depeyrot, Dolphin Integration's Chairman, said at the time. "As connected devices sleep most of their time, users of 22FDX also benefit from our ultra-low power and accurate oscillators to design an always-on RTC which consumes as little as 60 nA." See the Dolphin Integration website for the full catalog of their IP, EDA and ASIC/SoC service offerings, including for GF's 22FDX.
Read More
Part 2 of this two-part piece examines the potential benefits to be realized by pairing human Subject Matter Experts with smart silicon assistants, and what these new arrangements mean for semiconductor device manufacturing. Part 1 explores best-practice perspectives on collecting and utilizing smart data in industries outside semiconductor manufacturing, one of the important takeaways from the Smart Manufacturing panel discussion at SEMI ASMC 2018. So what does this observation (i.e. the field of medicine, in what seems at first glance a big data environment, is really just clusters and clusters of loose small data connected by the collective neural network of highly trained doctors and their colleagues) mean for semiconductor manufacturing? We think it means we need to apply the same level of intense focus that we already devote to instrumented data collection and analytics in the fab to something more: we need to better capture the vast expertise of our engineering and operational talent in semiconductor manufacturing. We think we need to record what the subject matter experts (SMEs) in the fab see, hear, and think as they investigate yield excursions or machine-down problems. We need to effectively combine product, process, equipment and component subject matter expertise / subject matter experts (SME) with big data analytics to more effectively solve manufacturing problems, be they killer or be they chronic. And we must provide structured methods for incorporating inputs from and active participation of SMEs throughout the data analysis lifecycle, from collection and aggregation, through filtering, feature extraction, analysis and optimization. Some of the challenge will be in just how do we make it easy to gather information from SMEs in real time, while standing in front of equipment in the fab. Internet of Things (Iot) devices are emerging to capture and label images and sounds to enable machine learning algorithms to recognize and help diagnose manufacturing problems based on sight and sound, complementing the instrumented data. But we also need to record the thought processes our human SMEs go through in those investigations – perhaps by the SMEs talking to a smart AI-based conversational assistant who helps make “rounds.” Doing contextual analysis on this added data, combined with the instrumented data, will create the equation Human + Machine = AI (Awesome Insight). Sounds reasonable, right? We think artificial intelligence becomes too artificial if you leave the human out of the equation. AI should be augmented intelligence, where we take the expertise and creativity of the human, and combine it with the rapid computational capabilities of the computer, in order to put problem identification and solutions on steroids. But with the already huge advancements to date in data analytics, cloud, and the emergence of AI, why do improvements in quality, machine utilization, and the implementation of predictive analytics in semiconductor manufacturing seem to be creeping along incrementally, and not appearing as dramatic, step-function improvements? Call it Smart Manufacturing, call it Connected Enterprise, call it Advanced Manufacturing, or Analytics, or Cloud, or the Digital Twin … there are no shortages of terms, philosophies, and technologies available, but why aren’t we seeing their rapid adoption? It could be it’s the downside that comes with needing people. “Good business leaders create a vision, articulate the vision, passionately own the vision, and relentlessly drive it to completion.” Jack Welch. We see from other industries that smart manufacturing conversations originating with the executives of a company thinking to implement smart manufacturing programs lead to vision; however, we also see from other industries, and from our own, that realizing this vision has often been a challenge. Why is that? One reason may be that the people who are personally vested in solutions they implemented in the past, as well as those who follow a pattern of ‘how we’ve always done things’, create, inadvertently or not, persistent internal barriers hindering innovative action. Another may be that engagements with the working engineers and managers charged to be smart manufacturing implementers leads to the pursuit of low-hanging fruit, and cautious investments, that often utilize solutions that ultimately cannot scale and integrate. Not to mention the disadvantage of dealing with the legacy equipment, the legacy networks, the traditional thinking, and the lack of consistency in metrics adding to the confusion. Addressing all these barriers requires an alignment in strategy and execution, along with a plan to support the overall vision, often across the entire enterprise, which is no small matter. And then there are the standards. Having and adhering to standards in control solutions, networks, and data becomes critical in achieving real benefits from smart manufacturing. And data security. One of the other big impediments in the smart manufacturing transformation is data and IP security, another key concern (maybe the most significant) preventing us from moving forward more quickly (e.g. to cloud-based solutions) in our industry. More about that in a follow-up. Achieving synergy across all of manufacturing, from connecting equipment horizontally, through the production system (machines processes), and vertically, through enterprise systems and across production facilities, can only occur if we build standards, security, infrastructure, and human engagement throughout our ecosystem and supply chain. In simple form, the steps to do so include connecting assets, collecting and contextualizing data, and then driving business transformation with actionable insights gained from the data. With impact on every function, and every person, in the enterprise, from equipment operators in the fab through the C-Suite in HQ. Maintenance, Engineering, R D, Operations, Scheduling, IT, Procurement, Finance, HR all contribute, collaborate and benefit. Regardless of the technology, from device level analytics to predictive maintenance and optimization, the people that reside in these disparate groups need to come together with the smart machines to create a common strategy to achieve transformational results. Aligning an enterprise’s goals with its human capital is paramount to success. Therefore, we must challenge our team members and ourselves to work outside our comfort zones, and we need to be forever aware of the need for us to grow with the technology. Smart manufacturing is not necessarily about having fewer people in the fab, but it does suggest having people in the fab, perhaps with different, or upgraded, skill sets, who are even more efficient in their roles as a result of the boost they are getting from Industry 4.0. Fortunately, we now have techniques that let us combine the best, brightest, and latest and greatest analytics with our invaluable SMEs throughout the data analysis lifecycle. We’ll not only be able to deliver higher quality semiconductor manufacturing solutions all in all, but we’ll also be providing methods to more easily distribute, scale, maintain, and continually refine those hard-earned solutions. We expect that subject matter experts will continue to put the “smart” in machine-based smart manufacturing today, and for the foreseeable future. SME contributions are not an option, but, rather, an imperative for ensuring a semiconductor manufacturer’s sustained prosperity, much less its survival. Nancy Greco (IBM Watson), Dave Mayewski (Rockwell Automation), James Moyne (University of Michigan / Applied Materials), and Paul Werbaneth (Intevac, Inc.), along with Julie Jacob (Ernst Young), and Carson Henry (Micron Technology), were members of the SEMI ASMC 2018 panel discussing Industry 4.0 and the Future of Commercial Semiconductor Device Manufacturing. All opinions here are purely our own. Please contact Paul Werbaneth via email at [email protected]. The SEMICON West (July 9-11, 2018, in San Francisco) Smart Manufacturing Pavilion features working production equipment on the floor and three full days of speakers providing insights on building the infrastructure needed to enable AI. Equipment from Bosch Rexroth, Cimetrix, Rudolph Technologies, INFICON, Final Phase Systems, OMRON, DISCO and Edwards Vacuum will showcase cutting-edge smart manufacturing technologies. For information on the SEMI Smart Manufacturing initiative and how to get involved, please click here.
Read More
The CPUs in Summit, the world's new fastest supercomputer are built on 14nm FinFET-on-SOI technology. Yes, those IBM Power9 CPUs are fabbed by GlobalFoundries (you'll also find them in the z14, the most recent in IBM's z-series of servers – a series that's been on various iterations of SOI since its launch in 2003, btw). Summit's at the U.S. Department of Energy’s Oak Ridge National Laboratory (ORNL) in Tennessee, USA. It is now the top US supercomputer, and it's for science. The IBM-built Summit currently claims the spot in the Top500 as the world's smartest and most powerful supercomputer. “It is capable of performing 200 quadrillion calculations per second — or 200 petaflops — making it the fastest in the world,” says IBM's Dr. John E. Kelly, III, SVP, Cognitive Solutions and IBM Research. “But this system has never been just about speed. Summit is also optimized for AI in a data-intense world. We designed a whole new heterogeneous architecture that integrates the robust data analysis of powerful IBM Power CPUs with the deep learning capabilities of GPUs. The result is unparalleled performance on critical new applications.” And if that's not impressive enough for you, it's also #5 on the Green500 list for the world's most energy-efficient computers, posting Power Efficiency (GFlops/watts) of 13.889. [caption id="attachment_11940" align="alignright" width="300"] Summit supercomputer nodes: The IBM-built Summit supercomputer is the world's smartest and most powerful AI machine. It consists of 4,600 individual nodes. Each node contains two 22-core 3.07GHz IBM POWER9 CPUs, which are built on GlobalFoundries' 14nm HP FinFET-on-SOI technology, as well as six NVIDIA Telsa GPUs. (Photo Credit: ORNL).[/caption] As GF noted when they announced the technology in the fall of 2017 (read the GF press release here), their 14HP is the industry’s only technology to integrate a FinFET transistor architecture on SOI. Featuring a 17-layer metal stack and more than eight billion transistors per chip, the technology leverages embedded DRAM and other innovative features to deliver higher performance, reduced energy, and better area scaling over previous generations to address a wide range of deep computing workloads. These technologies have long, deep histories (and were developed in close collaboration with SOI wafer leader Soitec). Here at ASN we have a fabulous archive of pieces contributed by IBM explaining the genesis of the technology – they're great reads and still entirely pertinent: FinFET on SOI: Potential Becomes Reality (by T.B. (Terry) Hook et al, 2013) – this presents the key technical data. IBM: Why Fin-on-Oxide (FOx/SOI) Is Well-Positioned to Deliver Optimal FinFET Value (by Terry Hook, 2012) – this great piece busts myths and clearly explains why FinFETs on SOI deliver top performance. IBM: FinFET Isolation Considerations and Ramifications – Bulk vs. SOI (by Terry Hook, 2013) – explains why and how SOI increases operating voltage range, simplifies processing, reduces variation, lowers soft error rate, and enables higher circuit density. Embedded Memories in SOI – (by Subramanian S. Iyer, 2006) explains the importance of SOI in the memory part of the chip design equation. [caption id="attachment_11939" align="alignleft" width="300"] The IBM POWER9 processor delivers unprecedented speeds for deep learning and AI workloads. IBM Engineer, Stefanie Chiras tests the IBM Power System server in Austin, Texas. (Photo Credit: Jack Plunkett/Feature Photo Service for IBM).[/caption] As ORNL noted in its press release (you can read it here), the first projects will apply machine learning and AI to astrophysics, materials science, cancer research and systems biology. BTW, Summit also has a slightly smaller sister machine called Sierra, going in at the Lawrence Livermore National Laboratory (part of the Department of Energy's National Nuclear Security Administration). With 4,320 nodes (each also containing two 22-core 3.07GHz IBM POWER9 CPUs, which are built on GlobalFoundries' 14nm HP FinFET-on-SOI technology, but just four NVIDIA Telsa GPUs), Sierra's claimed the #3 spot on the June 2018 Top500 list of the world's most powerful supercomputers. And the Power 9 is now finding it's way into major data centers – like Google's (read about that here). There have been some good pieces in the press about it, including in Forbes and The Motley Fool. So yes, clearly there are exciting markets for FinFETs on SOI!
Read More
Part 1 of this two-part piece explores best-practice perspectives on collecting and utilizing smart data in industries outside semiconductor manufacturing, one of the important takeaways from the Smart Manufacturing panel discussion at SEMI ASMC 2018. Part 2 examines the potential benefits to be realized by pairing human Subject Matter Experts with smart silicon assistants, and what these new arrangements mean for semiconductor device manufacturing. The spacecraft Discovery and its HAL 9000 computer system had a digital twin. Did you know? Stanley Kubrick’s seminal film “2001: A Space Odyssey” had its theatrical release 50 years ago this April. “2001” isn’t just a great science fiction film. Rather, it’s a great work of cinema overall, across any category. (The American Film Institute lists “2001” as #15 in the AFI Top 100; a bit below “Vertigo,” a bit above “It’s A Wonderful Life.”) It’s a film so distinguished and so prescient that its lessons can inform our thinking about smart manufacturing, Industry 4.0, and artificial intelligence (AI) today. Not to give too much away, but the earth-bound digital twin of Discovery / HAL identifies a diagnostic error the onboard, Jupiter-bound HAL 9000 has made, things go awry from there, and one of the mission pilots, astronaut Dave Bowman, is forced to intervene. At the recent SEMI Advanced Semiconductor Manufacturing Conference, ASMC 2018, on 02 May 2018 in Saratoga Springs, NY, five diverse panelists representing capital equipment, IDMs, academia, the semiconductor supply chain, and smart manufacturing best practices outside the semiconductor industry engaged in a lively discussion with the ASMC attendees. They explored where “smart” is in our industry today, where it’s headed, and what that’s going to mean for us -- the professionals who have brought semiconductor manufacturing to the current state of smart, and are looking to implement an ever-smarter tomorrow. Not to give too much away, but the panelists and audience agreed that there’s nothing artificial about pairing human intelligence with machine-based smart manufacturing. Implementing an ever-smarter tomorrow in semiconductor manufacturing requires smart people just as much as it requires smart machines. Moving towards “smart” means understanding how to derive useful information and actionable intelligence from the ever-increasing pool of big data created during semiconductor manufacturing. Modern manufacturing sites are extensively instrumented today, and create massive amounts of data to consume, decipher, base decisions upon, or discard. As we dig into this problem we realize that equipment and processes in our industry are both obviously complex, but, also, subtly complex. Semiconductor manufacturing tools easily contain 100s to 1000s of components working together to produce nanometer scale, angstrom scale, or even atomic scale features using complex chemical, physical, and plasma processes. There is a plethora of potential failure points and modes, and despite our best efforts to collect more data, many processes continue to be only poorly observable. On top of that, semiconductor fabrication processes are always drifting, and the operational context is continually changing as we change product mix, process maintenance swap-out kit components, and operating conditions and recipes. Sounds like … hospitals, and healthcare? When you see your doctor, she will collect and look at your instrumented data – blood work, blood pressure, weight, and other quantifiable factors. But, typically, your doctor won’t draw a conclusion based on that analysis alone. Rather, your doctor will sit with you, ask probing questions, and record what she asked, your responses, and what she saw, what she heard, and what she thought. Then she’ll build a hypothesis, combining the “anecdotal” data with the instrumented data, and derive from that data set both a likely diagnosis and an effective course of action. In this case, beyond the instrumented data, two humans, and their natural language input, are part of the equation: the patient, with his observations and thoughts, as well as the doctor, with hers. And it’s been a formula for success. Healthcare has made huge, step-function improvements across a spectrum of deadly diseases, as well as with less-deadly chronic afflictions, by harvesting this complex input, committing the proven disease presentation – disease diagnosis – and disease treatment models to medicine’s collective memory, and then teaching the next generation of healthcare providers both the general methods and the standard protocols essential to maintaining good health and successful outcomes. Maybe, in medicine, what seems a big data environment is really just clusters and clusters of loose small data connected by the collective neural network of highly trained doctors and their colleagues. Nancy Greco (IBM Watson), Dave Mayewski (Rockwell Automation), James Moyne (University of Michigan / Applied Materials), and Paul Werbaneth (Intevac, Inc.), along with Julie Jacob (Ernst Young), and Carson Henry (Micron Technology), were members of the SEMI ASMC 2018 panel discussing Industry 4.0 and the Future of Commercial Semiconductor Device Manufacturing. All opinions here are purely our own. Please contact Paul Werbaneth via email at [email protected]. The SEMICON West (July 9-11, 2018, in San Francisco) Smart Manufacturing Pavilion features working production equipment on the floor and three full days of speakers providing insights on building the infrastructure needed to enable AI. Equipment from Bosch Rexroth, Cimetrix, Rudolph Technologies, INFICON, Final Phase Systems, OMRON, DISCO and Edwards Vacuum will showcase cutting-edge smart manufacturing technologies. For information on the SEMI Smart Manufacturing initiative and how to get involved, please click here.
Read More
The MCU at the heart of Sony's new smart-sensing SPRESENSE™ for IoT is built on FD-SOI. Why? Low operating voltage and low power consumption, of course! Sony's got two cool new products going on sale in July 2018: the SPRESENCE main and extension boards for IoT applications, equipped with a smart-sensing processor (read the full press release here). A CXD5602PWBCAM1 camera board for sensing cameras will go on sale in August. All were on display at the SF Maker Fair '18, where they were an instant hit. [caption id="attachment_11931" align="alignright" width="300"] Here are the main features of Sony's CXD5602 MCU for IoT, which is built on FD-SOI. (Courtesy: Sony Semiconductor Solutions)[/caption] The main board (it's open source, btw) will run about US$50. You'll find the specs and main features here. Spresense is powered by Sony's FDSOI-based CXD5602 MCU (ARM Cortex-M4F × 6 cores), with a clock speed up to 156 MHz. The main board utilizes a multi-CPU structure equipped with Sony's state-of-the-art GNSS (Global Navigation Satellite System – which they talked about at the most recent SOI Symposiums in SF and Tokyo) receiver. A variety of systems for diverse applications, including drones, smart speakers, sensing cameras and other IoT devices, can be built by combining these boards and developing the relevant applications. The new board can be used to control a drone, for example, using GPS positioning technology and a high-performance processor, voice-controlled smart speakers, low-power consumption sensing cameras and other IoT devices, etc. It can also be combined with various sensors for use in systems that detect errors in production lines on the factory floor.
Read More
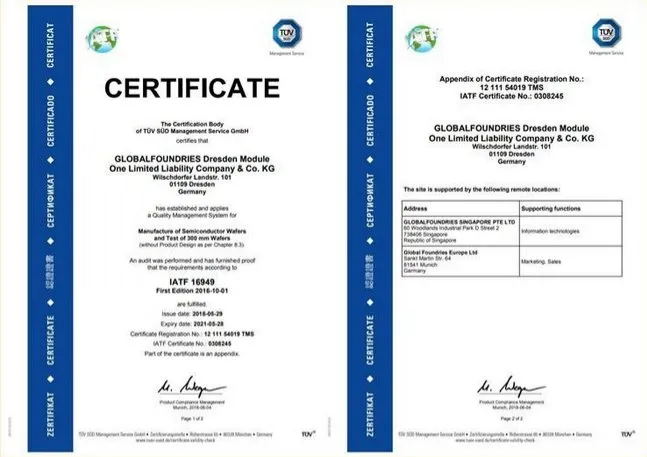
[caption id="attachment_11914" align="alignright" width="150"] Mark Granger, GlobalFoundries' VP Automotive Product Line Management[/caption] GF's 22FDX® (22nm FD-SOI) offering is on an automotive roll. The technology platform has been certified for several key automotive standards, and GF has announced an exciting new ADAS customer in Arbe Robotics. In addition to sharing info from various press releases and blogs, ASN also had a chance to catch up with Mark Granger, GF's VP for automotive, who provided some great insights. Read on! Taking the Heat When it comes to compliance, automotive industry standards are excruciatingly rigorous. Every part that goes into a car must adhere to the relevant standards: chips are no exception. One such standard is the AEC – Q100, a “Failure Mechanism Based Stress Test Qualification For Integrated Circuits”. The AEC – aka the Automotive Electronics Council – handles those testing standards and certification. Grade 2 means a technology is certified for the -40°C to +105°C ambient operating temperature range. To achieve Grade 2 certification, devices have to successfully withstand reliability stress tests for an extended period of time over the specified temperature range. GF recently announced that 22FDX has been AEC Q100 Grade 2 certified (press release here). However Granger adds that for their customers, they've added additional headroom that takes them to 125°C. They're now working on Grade 1 certification, he says, which means the devices are certified to handle junction temperatures up to 125°C (and there again, GF has added additional headroom that takes them to 150°C). That should be done by the end of 2018. The ability you get with FD-SOI to tune the transistors using body biasing is really beneficial here, he says. For GF, the 22FDX qualifications exemplifies their commitment to providing high-performance, high-quality technology solutions for the automotive industry. The automotive industry is driven by a “zero excursions – zero defects” mindset, says Granger, and that drives the foundry, too. SOI has been used for decades across industries where heat and electromagnetic radiation are challenges, bringing soft error rates (SER) down by orders of magnitude, notes Granger. (SOI, btw, essentially eliminates what are known as Single Event Upsets (SEU) caused by latch-up, which in turn brings down SER.) That in turn, ties into the FIT (failure in time) rate – and that's part of the ISO 26262 “Road vehicles – Functional safety” standard – where 22FDX is also certified. As a part of GF's AutoPro™ platform, 22FDX allows customers to easily migrate their automotive microcontrollers and ASSPs to a more advanced technology, while leveraging the significant area, performance and energy efficiency benefits over competing technologies. Moreover, the optimized platform offers high performance RF and mmWave capabilities for automotive radar applications and supports implementation of logic, Flash, non-volatile memory (NVM) in MCUs and high voltage devices to meet the unique requirements of in-vehicle ICs. GF's Fab 1 in Dresden, Germany (which is where they do 22FDX) also has achieved ISO-9001/IATF-16949 certification, which demonstrates that it is capable of meeting the stringent and evolving needs of the automotive industry. (IATF is the International Automotive Task Force. 16949 is a Quality Management System (QMS) certification specifically for the automotive sector.) Granger wrote a really informative blog on the GF website – you can read it here. It includes this graphic, indicating where in the car 22FDX-based parts are expected to go. [caption id="attachment_11913" align="alignleft" width="1000"] Here's how GF sees the applications for 22FDX and other chip technologies in automotive applications. (Courtesy: GlobalFoundries)[/caption] On Radar GF recently announced that Arbe Robotics selected 22FDX® as the process technology for its groundbreaking patented imaging radar. Arbe aims to achieve fully automated system capabilities and enable safer driving experiences for autonomous vehicles (read the press release here). As the first company to demonstrate ultra-high-resolution at a wide field of view, Arbe Robotics’ radar technology can detect pedestrians and obstacles at a range of 300 meters, in any weather and lighting conditions. The processor creates a full 3D shape of the objects and their velocity, and classifies targets using their radar signature. As Granger noted in his blog, “Radar is one of several sensor types used to detect objects near a vehicle, to enable features like adaptive cruise control. Lidar is another. It uses pulsed lasers to determine distance from an object by measuring the time it takes for the light to reflect back. However, lidar is currently expensive and is affected by weather conditions. Radar is less expensive, and higher-resolution radars promise to compete well with lidar in automotive applications, thereby enabling lower-priced vehicles to enjoy greater ADAS capabilities. 22FDX-based radar sensors can provide higher resolutions and less latency than current radar sensors at a very low total system cost.” While they may be complementary at first, there is a battle brewing between high-resolution radar and lidar, Granger told ASN. Putting their solution on 22FDX enables Arbe to achieve a 77 GHz mmWave radar and compete cost-effectively with lidar. “They wanted the best,” says Granger. 22FDX can achieve the requisite Ft and Fmax figures of merit. And with transistor stacking, they can also integrate the power amplifier (PA) on a single device. With the low inherent capacitance of the PA in 22FDX, you can get the high power output you need for mmWave but with low power consumption. GF blogger Dave Lammers has also written a great piece about the Arbe solution (you should read it: here's the link). “The company said its advanced technology allows the detection of small targets, such as a human or a bike even if they are somewhat masked by a large object such as a truck,” he writes. “The imaging radar can determine whether objects are moving, and in what direction, and alert the car in real-time about a risk. “While other car sensors can fail when it is raining, if there’s fog, and due to blinding lights such as a sudden reflection, Arbe’s radar is completely oblivious to all those factors. The custom designed radar processor creates a full real-time 4D image of the environment, and classifies targets using their radar signature.” Avi Bauer, Arbe's VP of R D, is now clearly an SOI fan. Lammers quotes him as saying, “With SOI the design is more straightforward, and (voltage) biasing allows you to do things that cannot be done in standard CMOS. For the transmit and receive modules, SOI’s higher resistivity substrate benefits the passive components – inductors and capacitors – and allows good isolation. High Q passives are important. At 22nm, SOI allows better performance overall.” Clearly good things are coming down the road for FD-SOI!
Read More
Self-driving cars have been all the rage in both the trade and popular press in recent years. I prefer the term “autonomous vehicles,” which more broadly captures the possibilities, encompassing not only small passenger vehicles but mass transit and industrial vehicles as well. Depending on who’s talking, we will all be riding in fully autonomous vehicles in five to 25 years.The five-year estimates come from startups eager to raise venture capital while the 25-year estimates stem from Tier 1 automotive suppliers who tend to be more conservative in outlook. Regardless of the timeframe, a multitude of investors – national governments, venture capitalists and companies – are dedicating significant capital and effort to make autonomous vehicles a reality.I must admit that I did not fully grasp the enthusiasm for self-driving cars until last year. First, I’ve always enjoyed driving, unless I’m in stop-and-go traffic, so I couldn’t imagine relinquishing the task. Second, I’ve deliberately arranged my life to spend minimal time in my car. However, traffic has become much heavier in my metropolitan area (Boston), and I know that many people in cities around the world face longer commutes and waste more time in gridlock.What is the solution to this problem that is only getting worse? I had an epiphany while walking through Shinigawa Station in Tokyo, one of the busiest train stations in the world. Dense streams of people crisscrossed the station on their individual paths, managing to avoid collisions without the aid of traffic controls. Evidently, humans have an innate collision-avoidance ability that makes traffic controls for pedestrian crowds unnecessary. If autonomous vehicles could achieve the same excellence in collision-avoidance, we could potentially reduce or eliminate traffic controls for vehicular traffic, providing a huge gain in transportation efficiency and relief from gridlock.Sensors as core building blocksNew and improved sensors, many based on micro-electromechanical systems (MEMS) technology, are key to achieving this vision. While MEMS inertial sensors (such as accelerometers and gyros) are already integral to the core safety systems in conventional vehicles, they are also essential to improved self-navigation in autonomous vehicles.The challenge for MEMS suppliers is to deliver inertial sensors that meet the requirements for self-navigation systems, which are different and more demanding than for safety systems.Pinpointing a vehicle’s position requires “dead reckoning” based on inertial sensor signals as a supplement to GPS input. Undesirable drift in the inertial sensor signals due to mechanical quadrature, temperature sensitivity and noise can quickly add up to a large error in position that may result in a collision. To meet the more rigorous requirements for autonomous vehicles, suppliers must design MEMS inertial sensors that are substantially more precise and resistant to drift. This requires design software that is both extremely accurate and fast, as well as increasingly precise and reliable manufacturing capabilities.Other MEMS-based devices, such as micromirrors and micro ultrasound transducers (MUTs), are also promising options for implementing vision and range-finding systems in autonomous vehicles. These sensing systems are needed for building electronic versions of the human collision-avoidance abilities that I witnessed in Shinigawa Station – and it is these systems that autonomous vehicles must emulate.When will self-driving cars become a reality? Aside from the provocative question that got you to read this far, I don’t have a definitive answer. It will undoubtedly occur in phases, ranging from the driver-augmentation systems available in today’s cars to the full autonomy and ubiquity that will allow reduction of traffic controls in 20 years or more. It is clear that the ultimate goals for autonomous vehicles are highly worthwhile, and that achieving those goals will require better-performing and more diverse MEMS sensors. Stephen (Steve) Breit, Ph.D. is Senior Director, MEMS Business, at Coventor, a Lam Research Company. Steve has been responsible for overseeing development and delivery of Coventor’s industry-leading software tools for MEMS design automation since joining Coventor in 2000. Steve holds numerous patents on software systems and methods for MEMS design automation and virtual fabrication. He holds a Ph.D. in Ocean Engineering from MIT and a B.S. in Naval Architecture and Marine Engineering from Webb Institute.For more information, visit: https://www.coventor.com
Read More